 Paljet
Forged Ring Gear, Converter Ring Gear, Trunnion & Sleeve
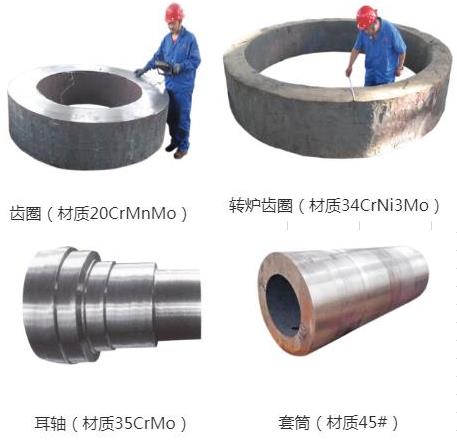
Forged ring gear, converter ring gear, trunnion and sleeve
Product Positioning & Application Fields
All products are monolithic heavy-duty forged components for metallurgical equipment. Continuous metal grain flow eliminates casting defects such as porosity and shrinkage, delivering high load capacity, impact resistance and fatigue resistance, widely used in steelmaking converters, heavy-duty reducers and metallurgical machinery.
20CrMnMo Ring Gear:
Carburizing gear steel. After carburizing and quenching, gear teeth have high surface wear resistance while the core retains high toughness, suitable for heavy-duty reducers, sintering and mining transmission systems.
34CrNi3Mo Converter Ring Gear:
Large cross-section alloy steel with superior hardenability, high strength and toughness against heavy impact and cyclic loads. It serves as the main drive large ring gear for converter tilting mechanism in steel plants.
35CrMo Trunnion:
Cr-Mo quenched & tempered steel with excellent torsion and fatigue resistance, stable mechanical properties under medium temperature. It is the key load-bearing shaft for steelmaking converters and ladle turrets under bending and torsion loads.
45# Sleeve:
High-quality carbon steel forging with good cost performance and stable mechanical properties, used as shaft bushing, spacer and protective sleeve for supporting and positioning.
Industries: Iron & steel metallurgy (converter, ladle equipment), mining, cement, heavy-duty reducers and heavy port machinery.
2. Process Capability Overview
General workflow: Billet cutting → segmented temperature-controlled heating → upsetting, drawing, ring rolling / open die forging (controlled forging ratio to align grain flow along force path) → post-forging annealing / normalizing for stress relief → rough machining → heat treatment → finish machining → NDT inspection.
Process highlights for each part.
20CrMnMo Ring Gear: Forged blank → rough turning → carburizing & quenching + low-temperature tempering → gear grinding for hard tooth surface and tough core.
34CrNi3Mo Converter Ring Gear: Large ring forging, stress relief annealing after forging. Quenching & tempering after rough machining, followed by hobbing and grinding. Slow heating & cooling to minimize heat distortion for large cross-section.
35CrMo Trunnion: Open die drawing forming, quenching & tempering. Optional surface hardening on journal. CNC turning, deep hole machining and cylindrical grinding with strict concentricity control.
45# Sleeve: Ring forging, normalizing or quenching & tempering. Precision turning and honing for inner & outer circle, to guarantee roundness and uniform wall thickness.
Capabilities.
Manufacture large ring gear, long trunnion shaft and forged sleeve. Deliver raw forging blanks, semi-finished or fully machined finished parts. Gear hobbing, grinding, cylindrical grinding, keyway and flange machining available. Heat treatment options: carburizing quenching, quenching & tempering, normalizing and annealing.
3. Quality Control & Inspection
Produced under ISO9001 system, full inspection from raw material to finished goods:
Raw material incoming: mill certificate review, PMI spectral analysis, strict control of S and P impurities.
In-process forging inspection: record of forging temperature, deformation and forging ratio; visual check for surface cracks and folds.
Heat treatment test: Brinell / Rockwell hardness test; tensile, impact and metallographic test from sample coupons.
Nondestructive testing: UT ultrasonic inspection for internal shrinkage, inclusion and internal defects; MT magnetic particle inspection for surface/subsurface cracks at tooth root and shaft journal. Critical parts such as converter ring gear and trunnion require 100% UT+MT, complying with GB, JB/T, ASTM or client specified standards.
Dimensional & geometric inspection: OD, ID, gear profile, concentricity, runout and wall thickness measured by precision gauges, gear tester or CMM.
Visual final inspection. Documents including MTR, heat treatment chart, NDT reports and dimensional records supplied with shipment.
4. Customization Process
Inquiry: Customer provides drawings or specs including dimensions, material grade, heat treatment, gear parameters, working load, hardness and NDT requirements.
Technical evaluation: Our factory reviews forging feasibility, recommends forging & heat treatment plan and issues quotation.
Technical confirmation: drawing, tolerance and acceptance criteria mutually agreed, technical contract signed.
Production schedule: billet cutting → forging → heat treatment → machining → gear cutting → NDT.
Final inspection: complete dimensional, mechanical and NDT tests, full quality documents prepared.
Packing & delivery: anti-rust protection, steel frame / wooden crate packing, sea or land transport, after-sales technical support available.
Note: The above information is reviewed by Engineer Song Enyu from PALJET.
Previous product:42CrMo Forged Wheels| Heavy Duty Rail Wheels