 Paljet
Composite HSS Roll & Indefinite Chill Cast Iron Roll | Hot Rolling Mill Work Rolls
Detailed Introduction
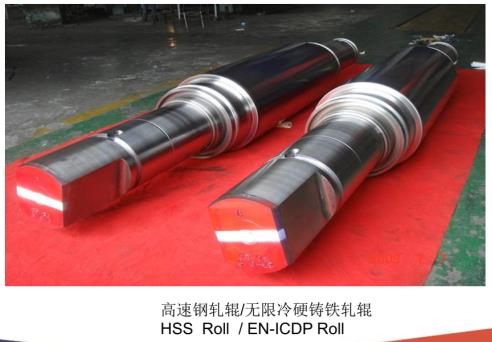
High speed steel composite work roll for hot rolling mill,
centrifugal cast HSS roll
1. Product Positioning & Application
HSS Roll and EN-ICDP Roll are composite work rolls for hot strip mill finishing stands, manufactured by horizontal centrifugal casting. They consist of a hard wear-resistant outer working layer and a tough ductile iron roll core, balancing high surface wear resistance and impact toughness.
HSS Roll (High Speed Steel Composite Roll): The outer shell adopts high-vanadium high-speed steel alloy with V, W, Mo, Cr elements. Its microstructure is tempered martensite plus hard MC carbides. It delivers superior wear resistance and thermal fatigue performance for heavy-load hot rolling.
EN-ICDP Roll (EN Indefinite Chill Double-Poured Roll): Alloy indefinite chill cast iron outer layer with bainitic/martensitic matrix and uniformly distributed fine graphite. It features excellent thermal crack resistance and anti-sticking property, producing good strip surface quality with optimized cost.
Product positioning: OEM composite rolls manufactured to EN, DIN and customer original drawings, fully interchangeable with imported hot mill work rolls for overseas mill revamping and spare part replacement. Applications: Hot strip mill finishing stands (HSS for F1-F4; EN-ICDP for F4-F7), Steckel mills, plate mill finishing stands. Target clients: overseas steel plants, metallurgical EPC contractors and rolling mill OEMs.
2. Manufacturing Capability Overview
Our factory produces composite rolls by horizontal centrifugal casting, with differentiated alloy formula and heat treatment for HSS and EN-ICDP grades: Alloy Melting: Medium frequency induction furnaces melt outer layer alloy and ductile iron core separately. Refining, deoxidation and degassing are performed to strictly control alloy composition and harmful S & P impurities. Centrifugal Double-Pour Composite Casting (Core Process): Metal mold rotates at high speed. The wear-resistant outer alloy is poured first and forms a dense working layer under centrifugal force. When the outer shell reaches semi-solid state, ductile iron for roll core is poured in the second stage to achieve sound metallurgical bonding and prevent interface delamination. Shakeout, Gating Removal & Rough Machining: Shakeout and riser cutting; rough turning of roll barrel and roll neck with grinding allowance reserved. Differentiated Heat Treatment: HSS Roll: Pre-annealing + high-temperature quenching + multiple tempering to optimize carbide morphology and improve hot hardness and spalling resistance. EN-ICDP Roll: Double tempering to reduce retained austenite, stabilize barrel hardness and restrain thermal crack propagation. Precision Grinding & Finishing: Dedicated roll grinders for barrel finish grinding with tight control of roundness, cylindricity and surface roughness; roll neck finish machining for bearing assembly.
3. Quality Control & Inspection
Full-process QC with third-party witness available, complying with European metallurgical roll specifications: Raw material inspection: Spectrometer sampling for alloys and pig iron; real-time composition monitoring during melting. Visual & dimensional inspection: Visual surface check; 3D laser scanning for roll geometry and tolerances. Non-destructive testing (NDT): UT ultrasonic inspection to detect internal shrinkage, inclusions and delamination at composite bonding interface. 100% PT penetrant inspection on roll barrel and neck for surface microcracks. Hardness, metallurgical & mechanical test: Multi-point Shore hardness test for barrel hardness uniformity. Metallographic examination for carbide and graphite morphology; tensile & impact tests to verify core toughness. Documentation: Material certificate, heat treatment report, UT & PT reports, hardness record and dimensional inspection report for export clearance. 4. Customization Process
Technical discussion: Client provides roll drawings, material grade (HSS / EN-ICDP), barrel hardness range, NDT class and dimensional tolerances. Our team reviews centrifugal casting feasibility and alloy formulation. Quotation & technical confirmation: Issue manufacturing plan, lead time and commercial quotation. Sign technical agreement and define inspection scope, witness points and acceptance criteria. Process design: Develop alloy formula, centrifugal rotation speed, pouring sequence and heat treatment procedure. Production & witness: Melting, centrifugal composite casting, heat treatment, machining and grinding. On-site witness by client or third-party inspectors is supported at key production stages. Final inspection, anti-rust treatment, packing & shipment: Complete full NDT, hardness and dimensional tests and deliver full quality documents. Apply anti-rust coating and export packing before ocean freight.
HSS Roll and EN-ICDP Roll are composite work rolls for hot strip mill finishing stands, manufactured by horizontal centrifugal casting. They consist of a hard wear-resistant outer working layer and a tough ductile iron roll core, balancing high surface wear resistance and impact toughness.
HSS Roll (High Speed Steel Composite Roll): The outer shell adopts high-vanadium high-speed steel alloy with V, W, Mo, Cr elements. Its microstructure is tempered martensite plus hard MC carbides. It delivers superior wear resistance and thermal fatigue performance for heavy-load hot rolling.
EN-ICDP Roll (EN Indefinite Chill Double-Poured Roll): Alloy indefinite chill cast iron outer layer with bainitic/martensitic matrix and uniformly distributed fine graphite. It features excellent thermal crack resistance and anti-sticking property, producing good strip surface quality with optimized cost.
Product positioning: OEM composite rolls manufactured to EN, DIN and customer original drawings, fully interchangeable with imported hot mill work rolls for overseas mill revamping and spare part replacement. Applications: Hot strip mill finishing stands (HSS for F1-F4; EN-ICDP for F4-F7), Steckel mills, plate mill finishing stands. Target clients: overseas steel plants, metallurgical EPC contractors and rolling mill OEMs.
2. Manufacturing Capability Overview
Our factory produces composite rolls by horizontal centrifugal casting, with differentiated alloy formula and heat treatment for HSS and EN-ICDP grades: Alloy Melting: Medium frequency induction furnaces melt outer layer alloy and ductile iron core separately. Refining, deoxidation and degassing are performed to strictly control alloy composition and harmful S & P impurities. Centrifugal Double-Pour Composite Casting (Core Process): Metal mold rotates at high speed. The wear-resistant outer alloy is poured first and forms a dense working layer under centrifugal force. When the outer shell reaches semi-solid state, ductile iron for roll core is poured in the second stage to achieve sound metallurgical bonding and prevent interface delamination. Shakeout, Gating Removal & Rough Machining: Shakeout and riser cutting; rough turning of roll barrel and roll neck with grinding allowance reserved. Differentiated Heat Treatment: HSS Roll: Pre-annealing + high-temperature quenching + multiple tempering to optimize carbide morphology and improve hot hardness and spalling resistance. EN-ICDP Roll: Double tempering to reduce retained austenite, stabilize barrel hardness and restrain thermal crack propagation. Precision Grinding & Finishing: Dedicated roll grinders for barrel finish grinding with tight control of roundness, cylindricity and surface roughness; roll neck finish machining for bearing assembly.
3. Quality Control & Inspection
Full-process QC with third-party witness available, complying with European metallurgical roll specifications: Raw material inspection: Spectrometer sampling for alloys and pig iron; real-time composition monitoring during melting. Visual & dimensional inspection: Visual surface check; 3D laser scanning for roll geometry and tolerances. Non-destructive testing (NDT): UT ultrasonic inspection to detect internal shrinkage, inclusions and delamination at composite bonding interface. 100% PT penetrant inspection on roll barrel and neck for surface microcracks. Hardness, metallurgical & mechanical test: Multi-point Shore hardness test for barrel hardness uniformity. Metallographic examination for carbide and graphite morphology; tensile & impact tests to verify core toughness. Documentation: Material certificate, heat treatment report, UT & PT reports, hardness record and dimensional inspection report for export clearance. 4. Customization Process
Technical discussion: Client provides roll drawings, material grade (HSS / EN-ICDP), barrel hardness range, NDT class and dimensional tolerances. Our team reviews centrifugal casting feasibility and alloy formulation. Quotation & technical confirmation: Issue manufacturing plan, lead time and commercial quotation. Sign technical agreement and define inspection scope, witness points and acceptance criteria. Process design: Develop alloy formula, centrifugal rotation speed, pouring sequence and heat treatment procedure. Production & witness: Melting, centrifugal composite casting, heat treatment, machining and grinding. On-site witness by client or third-party inspectors is supported at key production stages. Final inspection, anti-rust treatment, packing & shipment: Complete full NDT, hardness and dimensional tests and deliver full quality documents. Apply anti-rust coating and export packing before ocean freight.
Note: The above information is reviewed by Engineer Song Enyu from PALJET.
Next product:Hot Stove GratePrevious product:Forged Steel Backup Roll for Hot & Cold Rolling Mill
| Heavy Metallurgical OEM Rolls
Anshan Leibo Metallurgical Equipment Manufacturing Co., Ltd. Registered Address:Yanlangzhai Village, Dadaowan Town, Qianshan District, Anshan City, Liaoning Province, P.R.China . All Rights Reserved © 2026