 PALJET
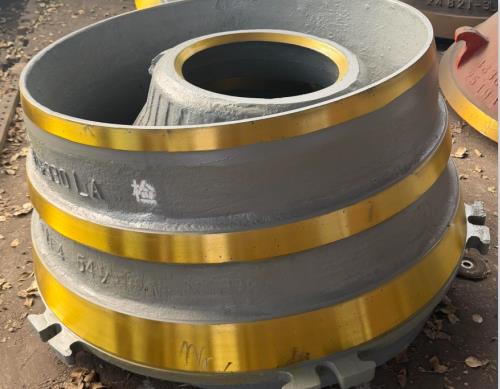
High Manganese Steel Cone Crusher Bowl Liner
High Manganese Steel Cone Crusher Bowl Liner
1. Product Positioning & Application Fields
The bowl liner is the core fixed cone wear part of cone crushers. It adopts high manganese steel grades including Mn13, Mn13Cr2 and Mn18Cr2. It relies on the unique work-hardening property of high manganese steel: under continuous extrusion and impact from materials, the working surface gets hardened with increased hardness, while the core of the casting maintains high toughness. It balances wear resistance and impact resistance to avoid cracking and chipping.
Product positioning: Wear-resistant castings specially used for secondary and tertiary crushing processes in mine and aggregate production lines. It can match mainstream spring cone, single-cylinder hydraulic and multi-cylinder hydraulic cone crusher models at home and abroad and support OEM replacement supply. Products are exported to Japan, South Korea, Southeast Asia and other overseas markets.
Application Fields: Metal ore mineral processing, sand and aggregate production, metallurgical raw material crushing, construction waste recycling and stone processing.
Applicable Materials: Granite, basalt, iron ore, copper ore, river pebble, diabase and other medium-to-high hardness ores and rocks.
Working Condition Features: Subjected to laminar extrusion and particle abrasive wear for secondary and tertiary crushing.
2. Manufacturing Capability Overview
Paljet adopts resin sand precision casting process for bowl liner production. It owns a complete production line covering casting, heat treatment and machining, equipped with medium-frequency melting furnaces, large heat treatment kilns, CNC vertical lathes, spectrometers and other equipment. The complete process flow is as follows:
Pattern Making and Moulding: Produce wood or resin patterns according to 2D drawings or 3D models; optimize gating and riser systems to reduce defects such as shrinkage cavity, porosity and slag inclusion.
Batching and Smelting: Select high-quality scrap steel, ferromanganese, ferrochrome and other alloy raw materials. Melting is carried out in medium-frequency furnaces. A spectrometer monitors the composition of molten steel in real time to ensure alloying elements including manganese, carbon and chromium meet standards.
Pouring and Controlled Cooling: Temperature-controlled pouring and staged slow cooling to reduce internal casting stress and prevent thermal cracks.
Sand Removal, Riser Cutting and Shot Blasting: Remove gating and risers; shot blasting eliminates oxide scale on casting surfaces, improves surface quality and exposes surface defects.
Water Toughening Heat Treatment (Core Process): Heat castings to 1040~1100℃ and hold for sufficient time to fully dissolve carbides into austenite, followed by rapid water quenching to obtain a full austenite matrix. This is the key to achieving the work-hardening performance of high manganese steel.
Finish Machining: Perform CNC machining on assembly mating surfaces, positioning surfaces and mounting bolt holes to guarantee dimensional accuracy and ensure proper fitting with the adjusting ring.
3. Quality Control & Inspection
The company follows the ISO9000 quality system and implements full-process traceable quality inspection from raw material incoming to finished product delivery.
Raw Material Incoming Inspection: Acceptance check for scrap steel and alloy materials; spectral composition recheck before smelting.
In-process Inspection: Continuous recording of melting & pouring temperature, heat treatment furnace temperature and holding time. Test coupons are cast together with each batch for mechanical property tests.
Finished Product Inspection Items
Visual inspection: Check surface casting defects such as cold shut, cracks, blowholes and slag inclusion.
Dimensional inspection: Use calipers and gauges to check overall dimensions and assembly tolerances.
Mechanical property test: Brinell hardness and impact toughness tests.
Non-destructive testing: Magnetic Particle Testing (MT) / Penetrant Testing (PT), focusing on surface microcracks on assembly areas and working surfaces.
Batch Archives: Complete production and inspection records are kept for each batch. Material certificates and inspection reports can be provided upon request.
4. Customization Process
OEM and ODM customized production is available for bowl liners of non-standard models and special working conditions:
Technical Communication: Customers provide crusher model, drawings, photos of physical samples and working condition parameters (ore hardness, feed size, output and wear problems).
Material Scheme Confirmation: Engineers evaluate working conditions and recommend standard Mn13 high manganese steel or modified Mn13Cr2 / Mn18Cr2 high manganese steel.
Quotation & Lead Time Confirmation: Issue formal quotation after technical review and confirm production cycle.
Mold Development: Manufacture patterns/molds for brand-new non-standard products.
Trial Casting & Sample Inspection: Produce trial samples, complete full inspection and issue inspection reports.
Mass Production: Start batch casting after customer approval of samples.
Final Inspection, Anti-rust Treatment, Packaging & Shipment: Re-inspection before delivery, anti-rust treatment, packaging and logistics arrangement.
Note: The above information is reviewed by Engineer Song Enyu from PALJET.
Next product:High Manganese Steel Jaw Crusher Jaw PlatePrevious product:Molten Iron Ladle | OEM Large Hot Metal Transfer Ladle