 Paljet
8-20t Ingot Molds|Paljet
8-20t Ingot Molds
1. Product Positioning & Application Fields
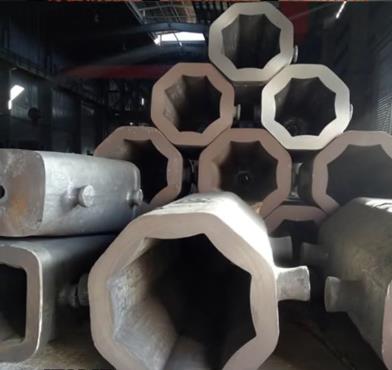
The 8-20 ton ingot molds are heavy casting toolings specially used for molten steel casting in metallurgical steelmaking. We supply ingot forming molds for large steelmaking and special steel forging enterprises. Available materials include ductile cast iron, heat-resistant cast iron and grey cast iron. Multiple inner cavity types are supported: square, round, multi-lobed and rectangular ingot profiles.
Our ingot molds are optimized for thermal fatigue resistance and thermal shock resistance, effectively reducing cracking and deformation under cyclic hot-cold working conditions to extend service life and cut customers’ overall metallurgy production cost. Both domestic bulk supply and OEM export orders are available.
Application Fields
Special steel melting plants: casting alloy steel, stainless steel, tool steel and bearing steel ingots
Heavy forging enterprises: pre-forming steel ingots for rolling mills and large forging blanks
Non-ferrous metal smelting and heavy industry material foundries
New metallurgical materials and special steel billet casting for military supporting projects
Product advantages: reasonably designed mold wall for excellent thermal stability and easy demolding. Equipped with lifting trunnions for convenient hoisting and transportation in steel workshops. Scrapped molds can be recycled and remelted with high material recycling rate.
2. Process Capability Overview
We adopt resin sand molding process for the production of 8–20 ton heavy ingot molds, with integrated capacity for heavy casting melting, pouring, heat treatment, cleaning and machining.
Full production workflow:
Process & pattern design: 3D modeling based on customer ingot drawings, solidification CAE simulation, pattern and core design with casting shrinkage allowance and riser feeding system.
Resin sand molding & core making: sand mixing, mold forming and core manufacturing. Assemble and close the mold.
Melting: Medium-frequency furnace melts pig iron, scrap steel and returns. Adjust composition for ductile iron / heat-resistant cast iron / grey cast iron; spheroidization and inoculation treatment for ductile iron to purify molten iron.
Pouring: Stable heavy casting pouring procedure with controlled temperature and speed to minimize shrinkage, porosity and cold shut defects.
Insulated cooling: Controlled cooling rate to reduce thermal stress and avoid early cracks of raw castings.
Shakeout & cleaning: shakeout, gate & riser cutting, shot blasting to remove burnt sand and oxide scale.
Stress-relief heat treatment: annealing to eliminate casting residual stress, stabilize dimensions and restrain in-service deformation.
Machining (on request): Planer and boring machine for inner cavity, end face and lifting lug machining to guarantee inner taper and dimensional precision.
Surface grinding and marking (heat number, specification, weight).
We accept prototype trial and mass orders, support customized ingot profiles. Equipped with heavy lifting & transportation equipment, we supply either raw blanks or fully machined finished ingot molds.
3. Quality Control & Inspection
Full-lifecycle product traceability in line with metallurgical acceptance standards. Third-party inspection is supported.
Raw material incoming inspection: chemical test for pig iron, scrap steel, alloy, resin sand, inoculant and nodulizer before storage.
Pre-furnace analysis: optical emission spectrometer to test molten iron chemical composition. Test coupons are reserved for each heat to guarantee material grade compliance.
In-process patrol inspection: sand mold strength test, mold assembly dimension verification, pouring temperature monitoring and cooling control.
Visual blank inspection: visual check plus magnifier to detect surface cracks, blowholes, sand sticking and cold shuts.
Non-destructive testing (on request): UT ultrasonic testing and MT magnetic particle inspection for internal and surface crack detection.
Physical & mechanical test: hardness test; metallographic nodularity inspection for ductile iron to verify strength and thermal fatigue performance.
Dimensional inspection: large calipers, custom gauges and large-scale measuring tools for inner cavity size, taper, wall thickness and trunnion position tolerance.
Final inspection, marking and warehousing. Batch inspection records are archived.
4. Customization Process
Technical communication: Customers provide finished ingot specifications, ingot shape (square / round / multi-lobed), ingot weight, material grade, inner taper, lifting structure, working conditions, order quantity and lead time. Our engineering team evaluates casting feasibility, runs solidification simulation, recommends material solution and provides quotation.
Process & pattern development: After confirmation, manufacture patterns and design sand cores with casting shrinkage allowance.
First article trial production: molding, melting and pouring to produce raw ingot mold casting, followed by heat treatment and machining as required.
Full first-article inspection & approval: dimensional measurement, material assay, hardness and NDT test with inspection reports. Customers confirm samples and we can adjust structure and wall thickness.
Mass production: Start mass manufacturing after sample approval. IPQC patrols the whole production process and stabilizes melting and pouring parameters.
Final inspection, protective packaging and shipment. Material certificates and inspection reports are delivered together with goods.
After-sales technical support: Track field service performance at steel mills, provide operation & maintenance advice, and optimize mold structure based on service life feedback
Note: The above information is reviewed by Engineer Song Enyu from PALJET.
Next product: Centrifugal Alloy Cast TubesPrevious product:Cast Iron Housings by Resin Coated Sand Process