 Paljet
1780 Hot Rolling Mill Housing / Mill Stand – Heavy Machinery OEM Cast Steel Mill Housing
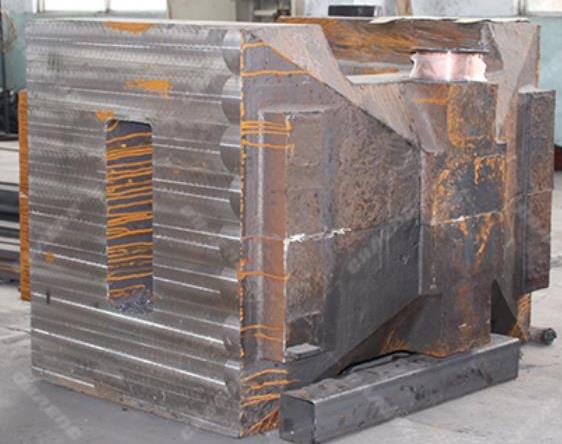
1780 hot rolling mill housing cast steel frame,
large heavy mill stand for hot strip rolling line, Heavy Machinery OEM
# 1. Product Positioning & Application Fields
The 1780 hot rolling mill housing is the core load-bearing frame for the finishing stand of the 1780mm hot strip mill, classified as high-end heavy cast steel metallurgical equipment. The housing bears huge alternating rolling force during full rolling conditions, supports work rolls, backup rolls, screwdown devices, chocks and the complete roll system. It acts as the backbone of the hot rolling line and determines mill rigidity, rolling stability and the flatness precision of finished steel strips.
**Application Fields**
- 1780mm wide hot strip production lines for carbon steel and low-alloy steel
- New hot rolling mill construction, spare housing replacement and technical revamping projects for steel plants
Service conditions: Long-term operation under alternating rolling load up to 40,000 kN, with high temperature, dust and impact loads. High rigidity, low residual stress and freedom from internal casting defects are mandatory.
# 2. Process Capability Overview
1. Casting simulation & process design
Casting simulation software such as MAGMA is adopted to simulate molten steel filling, solidification, shrinkage and temperature field distribution. Risers, chills and multi-ladle pouring scheme are optimized to predict risks of shrinkage cavity, porosity and cracking, and finalize the synchronous multi-ladle pouring process.
2. Smelting and multi-ladle combined pouring
Molten steel is refined in large-capacity ladles to strictly control harmful elements such as sulfur and phosphorus for improved steel purity. Six ladles are used for synchronous combined pouring, delivering a total molten steel weight of 314 tons. Rapid cavity filling is completed within a short time to avoid cold shut and inclusion defects.
3. Shakeout, riser cutting & primary heat treatment
Natural aging plus stress-relief annealing is performed to eliminate casting residual stress and prevent deformation and cracking during subsequent machining and service. Preliminary UT inspection is carried out after heat treatment.
4. Heavy-duty CNC machining
Large floor boring & milling machines and gantry milling machines are deployed for machining of housing window, chock mating surfaces, screwdown nut mounting surfaces and foundation reference surfaces. Tight control of geometric tolerances, flatness, parallelism and window perpendicularity is implemented.
5. Secondary stress-relief heat treatment
Secondary stress relief is conducted after semi-finishing to remove machining stress and guarantee dimensional stability during long-term operation.
6. Surface treatment and coating
Blasting is applied to achieve required surface cleanliness. A heavy-duty anti-corrosion coating system including primer, intermediate coat and topcoat is applied for wear and high-temperature resistance, adapting to high-temperature and humid working environments inside steel mills.
# 3. Quality Control & Inspection
Full-lifecycle traceability is implemented for material, smelting, heat treatment, NDT and dimensional records. The product complies with industrial standards for heavy cast steel components and can meet overseas specifications such as ASME and DIN upon client request.
1. Raw material & smelting inspection: In-situ spectroscopic analysis during melting and re-verification of chemical composition for finished castings. Mechanical property tests including tensile, impact and hardness tests are performed on test coupons.
2. Non-Destructive Testing (NDT)
- UT (Ultrasonic Testing): Applied on high-stress sections including window areas to detect internal shrinkage, porosity, cracks and inclusions.
- MT (Magnetic Particle Testing) / PT (Penetrant Testing): Performed on all critical working surfaces to detect surface and near-surface cracks.
3. Dimensional & geometric accuracy inspection
Laser trackers and large-scale measuring tools are combined to inspect window parallelism, perpendicularity, flatness of all reference surfaces and position of anchor holes. Full dimensional reports are documented.
4. Residual stress inspection & witness test: Sampling inspection of residual stress. Third-party witnessing inspection is available upon customer request.
5. Final delivery document package: Material certificates, heat treatment curves, NDT reports, dimensional inspection records and coating inspection logs.
# 4. Customization Process
1. Requirement discussion & technical input
Customer provides mill drawings, rolling force parameters, material specifications, applicable standards, NDT acceptance level, inspection specifications and service conditions. Our engineering team conducts technical review to verify manufacturing feasibility.
2. Technical agreement signing
Material grade, dimensional tolerances, NDT scope, inspection items, acceptance criteria, document delivery list and witnessing clauses are fully locked.
3. Process plan review
Internal review of casting simulation, pouring scheme, heat treatment curve, machining workflow and inspection plan. Critical plans will be submitted to customer for confirmation.
4. Manufacturing & in-process witnessing
Production flow: Smelting → pouring → heat treatment → rough machining → secondary heat treatment → finishing. Customer or third-party inspectors may carry out on-site witnessing at key nodes: pouring, heat treatment, NDT and dimensional recheck.
5. Final factory inspection & document acceptance
Full NDT and dimensional re-verification. All technical documents are audited before customer’s factory acceptance and release approval.
6. Coating, packaging & heavy cargo shipment
Protective packaging and cargo securing for ocean shipment. Full set of origin documents, material certificates, NDT and inspection reports are delivered.
Note: The above information is reviewed by Engineer Song Enyu from PALJET.
Next product: Molten Iron LadlePrevious product:Extra-Large Flat-Oval Eccentric Slag Pot for Japan Project
|Heavy Machinery OEM