 Paljet
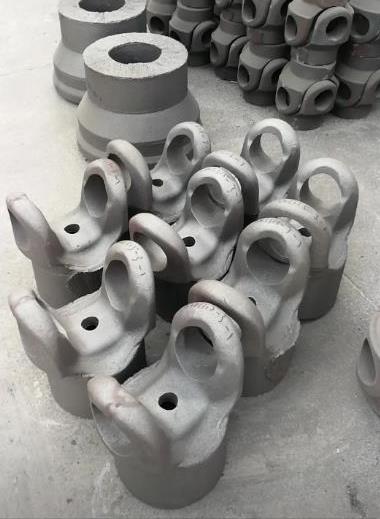
Lost Foam Cast Universal Joint Yoke Castings
Lost Foam Cast Universal Joint Yoke Castings
1. Product Positioning & Application Fields
Lost foam cast universal joint yoke castings are core load-bearing components for heavy-duty universal couplings, manufactured by lost foam (evaporative pattern) casting technology. Positioned as near-net-shape high-strength cast steel / low alloy cast steel blanks with no parting lines and high dimensional accuracy. The process delivers superior surface finish compared with conventional sand casting. Workpieces can be further processed by CNC machining and heat treatment to withstand high torque and alternating impact loads.
Typical applications include transmission shafts for metallurgical production lines, heavy mining equipment, construction machinery, heavy conveying systems, auxiliary wind power transmission, petroleum machinery and heavy vehicle transmission assemblies. We provide OEM castings for steel mills, mines and heavy machinery manufacturers as a replacement for imported universal joint yokes. Lost foam casting effectively reduces porosity and sand sticking defects, mitigates fatigue cracking and fracture risks under cyclic loads, and supports stable mass supply.
2. Process Capability Overview
Paljet Technology provides integrated services including lost foam casting, heat treatment and precision CNC machining for universal joint yokes.
EPS foam pattern fabrication: Produce 1:1 foam patterns according to customer drawings with reserved shrinkage allowance. Assemble gating and riser systems to form pattern clusters.
Refractory coating & drying: Dip the pattern cluster in high-temperature refractory coating, followed by staged full drying to prevent porosity and slag inclusion during pouring.
Flask loading, dry sand filling and vibration compaction: Place coated foam clusters into flasks, fill with unbonded dry silica sand, and compact by vibration tables to fully fill complex cavities of the yoke.
Vacuum-assisted pouring: Seal the flask and activate negative pressure. Molten steel is melted in medium-frequency induction furnaces with controlled pouring temperature and speed. High-temperature metal vaporizes foam patterns and replaces the space to form castings.
Cooling, shakeout and sand reclamation: Release vacuum after solidification, shake out castings; dry sand is recycled for repeated use.
Post-processing: Cut off gates and risers, perform shot blasting.
Heat treatment: Normalizing or quenching & tempering to release casting stress, optimize microstructure and improve strength and impact toughness.
CNC precision machining: Machine yoke bores, end faces and reference surfaces to meet geometric tolerances. Anti-rust treatment is available upon request.
Available materials include ZG45 and low-alloy high-strength cast steel. The process is suitable for small to large batch production of yokes with complex structures and smaller machining allowance.
3. Quality Control & Inspection
We implement full-lifecycle quality traceability from raw material incoming inspection to finished product delivery.
Raw material inspection: Spectral analysis for scrap steel and alloy additives, material certificate verification.
On-furnace test: Real-time spectral analysis during melting to adjust alloy composition and guarantee each heat meets specifications.
Foam pattern & coating inspection: Check foam dimension, coating thickness and drying status to prevent potential casting defects.
Visual inspection of blanks to identify surface defects such as porosity, cracks, cold shuts and inclusions.
Non-destructive testing: UT ultrasonic testing and MT magnetic particle testing to detect internal and surface cracks.
Sampling mechanical tests: Tensile test, impact test and hardness test.
Dimensional inspection: Calipers, micrometers and CMM to verify bore size, center distance and geometric tolerances.
Shipment documentation: Material certificates, NDT reports, heat treatment records and dimensional inspection reports are issued. Batch records are archived for full traceability. Third-party inspection by SGS / TÜV is supported.
4. Customization Process
Technical consultation: Customers provide 2D/3D drawings, material standards, mechanical requirements, NDT grade, quantity and lead time. Our engineering team evaluates lost foam casting feasibility, conducts structural optimization and provides quotation.
Casting simulation & foam mold development: CAE simulation for filling and solidification to optimize gating and riser design; manufacture foam molds for pattern production.
Prototype trial production: Fabricate foam clusters, coating and drying, vacuum pouring for first article blanks.
Full first-article inspection: Complete dimensional, material, mechanical and NDT tests, submit full sample inspection report for customer approval.
Mass production: After sample approval, start lost foam mass casting, heat treatment and CNC machining. IPQC inline inspection monitors critical parameters including vacuum level and pouring temperature.
Final inspection, packaging & shipment: Full inspection of finished goods, preparation of QC documents, anti-rust packaging and delivery.
After-sales technical support: Track field working conditions and optimize casting process based on customer feedback.
Note: The above information is reviewed by Engineer Song Enyu from PALJET.
Next product:Vibrating Screen Cast Alloy Screen PlatePrevious product:Wear & Heat Resistant Alloy Liners