 Paljet
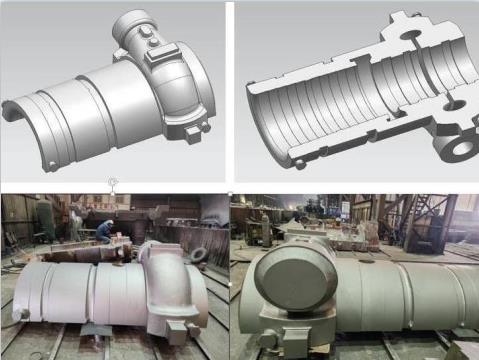
CB2 Material High Pressure Steam Turbine Casing
CB2 Material High Pressure Steam Turbine Casing
1. Product Position & Application
CB2 high-pressure steam turbine casing is the core high-temperature pressure-bearing casting for 620℃ ultra-supercritical reheat steam turbines. Material grade CB2 is ZG13Cr9Mo2Co1NiVNbNB (GX13CrMoCoVNbNB9-2-1), a 9%Cr martensitic heat-resistant cast steel with Co and B alloying. Liaoning Fu'an Heavy Industry has achieved mass production of CB2 high-pressure inner casing.
This alloy steel has high crack sensitivity and strict manufacturing requirements. It works continuously under high temperature and high pressure steam up to 620℃, requiring ultra-high steel purity, casting compactness, high-temperature creep strength and precise dimensional control. We deliver one-stop solution: raw casting, heat treatment, welding repair and precision CNC finish machining.
Application Scope
Main equipment supply for 620℃ reheat ultra-supercritical coal-fired steam turbine units (1000MW class high-pressure inner casing).
New high-efficiency thermal power plant construction, retrofitting and spare parts replacement.
Overseas thermal power EPC projects, complying with OEM specifications of mainstream turbine manufacturers.
Unit upgrade for thermal power plants to improve cycle efficiency and reduce carbon emission.
Compared with traditional 9Cr steel, CB2 steel is alloyed with Co, B, Nb and V, providing superior high-temperature creep rupture strength and oxidation resistance at 620℃. It is the landmark casting material for new generation high-efficiency thermal power units.
2. Manufacturing Capability Overview
CB2 alloy casting features high hot cracking tendency, easy oxidation and high risk of porosity & inclusion. Fu'an Heavy Industry adopts integrated workflow: MAGMA casting simulation, special melting, dedicated heat treatment, certified welding repair and large-scale CNC precision machining.
Digital casting simulation: 3D modelling and MAGMA filling & solidification simulation. Optimize gating, risers, chiller and anti-crack ribs specially for high-alloy CB2 steel, predict hot cracks, shrinkage and distortion.
Special melting & resin sand casting: Electric arc furnace + LF refining + VD vacuum degassing to strictly control H/O/N gas content and harmful impurities such as S, P, As, Sb. Resin sand moulding and core assembly, argon-shielded pouring and directional feeding to guarantee dense structure in pressure-bearing zones. Pouring temperature is tightly controlled within CB2 process window.
Custom multi-stage heat treatment: Special heat treatment cycle developed for CB2 martensitic heat-resistant steel, including normalizing, high-temperature tempering and stress relief annealing. Heating and cooling rates are precisely controlled to obtain qualified metallographic structure, eliminate casting stress and secure high-temperature creep performance. Attached test blocks are heat-treated together with casting body and cannot be cut off in advance.
Certified welding repair: Welders with CB2 material welding qualification perform defect repair. Preheating and dedicated post-weld heat treatment are applied to minimize residual welding stress and prevent reheat cracks.
Large multi-axis CNC precision machining: Large gantry milling and floor boring machines process split plane, flange, inner cavity, steam passage and bearing seat. Strict control on split surface flatness, bearing bore coaxiality and assembly step offset.
Casing pre-assembly: Trial fitting of upper and lower half casings, dimension recheck and clearance verification before shipment.
3. Quality Control & Inspection
Traceable quality management system conforming to ASME, JIS and OEM technical specifications. Witness inspection is available for customer or third-party surveyors at hold points.
Raw material & melting test: On-line spectral analysis during melting. Attached test blocks are sampled from casting body for chemical composition, tensile, yield, impact, hardness and 620℃ high-temperature creep rupture test. Gas content (H, O, N) and trace impurities are strictly limited.
Non-destructive testing (NDT): 100% UT, MT and PT inspection on pressure-bearing sections, split face and thick-wall areas under high-level acceptance criteria. RT inspection can be arranged upon request.
Precision dimensional inspection: Laser tracker and large CMM for full 3D scanning and geometric tolerance verification.
Pressure test: Hydrostatic test and air tightness test executed according to technical agreement to verify sealing performance under high temperature.
Complete quality documentation package: Melting records, heat treatment curves, NDT reports, dimensional reports, material certificates and high-temperature creep test reports. Full traceability for all production stages.
Final inspection: Visual examination, permanent marking, high-temperature resistant anti-corrosion coating and final review before shipment.
4. Customization Process
Technical discussion & review: Client provides turbine drawings and OEM specifications. We conduct special technical evaluation targeting CB2 requirements on melting, casting, heat treatment, NDT, tolerance and lead time, then sign technical agreement.
Quotation & contract signing: Formal quotation after technical confirmation. Contract defines witness inspection, hold points, acceptance standards, delivery and warranty terms.
Process planning & simulation: Internal process development, MAGMA solidification simulation, tooling and anti-crack structure design.
Production & in-process hold-point inspection: Moulding, melting & pouring, heat treatment, welding repair, rough & finish machining. Key stages open for customer witness inspection.
Final inspection & pre-assembly: Mechanical test, full NDT and 3D dimensional inspection; pre-assembly of upper and lower casing halves and report issuance.
Document handover & oversize shipment: Transfer of complete quality data package; heavy-duty anti-rust protection and dedicated packaging for oversize cargo. Shipment supervision optional.
After-sales service: Technical consultation for site assembly and quality support during warranty period.
Note: The above information is released by Angang Heavy Machinery and reviewed by Engineer Song Enyu from PALJET.
Next product:Integral Cast Turbine RunnerPrevious product:Mitsubishi Steam Turbine HP-IP Outer Casing Casting