 Paljet
Integrally Cast Water Turbine Runner |Paljet Heavy Equipment Parts
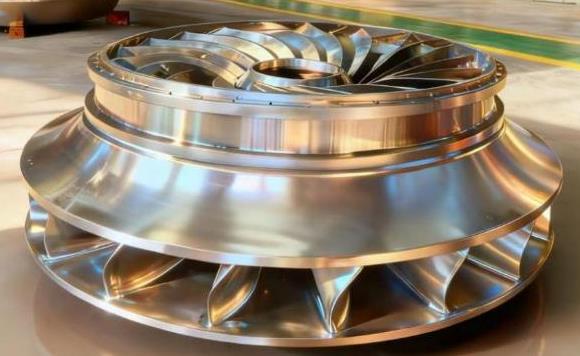
Integrally cast water turbine runner,
one-piece stainless steel Francis turbine runner for hydropower station
1. Product Position & Application
The integrally cast water turbine runner is the core rotating component for Francis hydro turbines. The crown, blades and band are cast in one single piece, eliminating welded joints between blades and crown/band. This design greatly reduces risks of welding cracks and fatigue failure, delivers smooth continuous hydraulic profile and outstanding cavitation & wear resistance. It is an advanced upgrade solution for medium & small hydropower units.
Made of ZG0Cr13Ni4Mo martensitic stainless steel, the runner features excellent cavitation resistance and silt wear resistance. As a GE Hydro qualified supplier, Fu'an Heavy Industry has delivered integrally cast runners for overseas hydropower projects such as Armenia Argel Hydropower Station. We supply full turnkey service: casting, 5-axis CNC hydraulic surface machining and static balance test.
Application Scope
New medium & small Francis hydropower stations worldwide
Old hydropower plant renovation & runner spare part replacement
Overseas hydropower EPC projects & renewable energy equipment supply
Custom production complying with GE, Andritz and other international OEM specifications
2. Manufacturing Capability Overview
We adopt digital manufacturing workflow: MAGMA solidification simulation, 3D printed sand core and resin sand moulding for one-piece runner casting.
Digital simulation & sand core development: 3D hydraulic model imported into MAGMA software to simulate filling and solidification, predict shrinkage and hot cracks at blade transition zones. 3D printed complex sand cores accurately replicate the complex curved blade geometry to solve moulding challenges of narrow inter-blade flow passages.
Stainless steel melting: Electric arc furnace + LF/VD vacuum refining to minimize gas and inclusions for high-purity stainless steel castings.
One-piece resin sand mould casting: Crown, multiple blades and band poured integrally in a single casting process, no blade welding required.
Solution treatment and tempering: Optimize metallographic structure, improve strength, toughness and cavitation resistance, release casting stress and reduce machining deformation.
Qualified repair welding: Local defect repair by certified welders followed by post-weld heat treatment in compliance with hydropower standards.
5-axis CNC precision machining: 5-axis machining centers for finish machining and polishing of blade hydraulic surfaces, crown and band. Static balance test after machining.
3. Quality Control & Inspection
Full traceable quality management system complying with ASME, IEC and GB/T hydropower casting standards. Our laboratory holds CNAS accreditation. Witness inspection is available for customers and third-party surveyors.
Raw material & melting inspection: Spectral analysis during melting; mechanical tests (tensile, yield, impact, hardness) on test blocks and casting samples.
Non-destructive testing (NDT): 100% UT, MT and PT inspection on blades, crown and band; RT inspection available on request to detect internal defects.
3D dimensional scanning: Laser tracker or CMM to scan blade curved surfaces and verify hydraulic profile tolerances.
Static balance test: Static balancing performed after finish machining to meet rotor unbalance requirements for water turbines.
Complete quality documentation package: Melting records, heat treatment curves, NDT reports, 3D inspection reports and material certificates. Full production traceability.
Final inspection: Visual examination, surface polishing, marking and anti-corrosion protection before shipment.
4. Customization Process
Technical discussion & review: Client provides hydraulic drawings, performance parameters and technical specifications. We evaluate material, blade quantity, profile tolerance, NDT requirements and lead time, then sign the technical agreement.
Quotation & contract signing: Formal quotation after technical confirmation. Contract defines witness inspection, packaging, transport and warranty terms.
Process simulation & tooling development: MAGMA solidification simulation, 3D printed sand core design and tooling planning.
Production & in-process hold-point inspection: Moulding, melting, integral casting, heat treatment, welding, rough & finish machining. Key stages open for customer witness.
Final inspection & static balance: Mechanical test, full NDT, 3D scanning and static balance test, issue full inspection reports.
Document handover, packaging & shipment: Transfer complete quality data package; heavy-duty anti-rust packaging for oversize cargo, sea shipment supervision optional.
After-sales support: Technical consultation for site assembly and quality response within warranty period.
Note: The above information is released by Angang Heavy Machinery and reviewed by Engineer Song Enyu from PALJET.
Next product:Locomotive Integral Cast Steel BogiePrevious product:CB2 Material High Pressure Steam Turbine Casing