 Paljet Pte Ltd Singapore
Integrally Cast Steel Locomotive Bogie Frame| Heavy Equipment Cast Parts
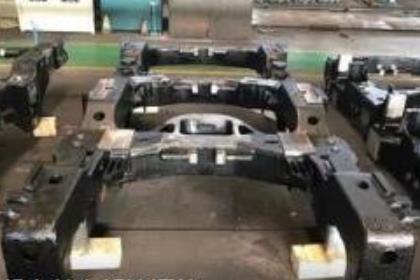
Integrally Cast Steel Locomotive Bogie Frame
1. Product Position & Application
Integrally cast steel locomotive bogie frame is the core load-carrying running component for heavy-duty freight locomotives. Manufactured by one-piece integral steel casting without welded splicing seams, it delivers superior overall strength, fatigue resistance and impact resistance compared with welded bogie frames.
Fabricated in compliance with AAR M-201 and international railway specifications, the bogie supports up to 35t axle load, with design service life of 20 years / 2 million km. It continuously bears alternating impact load, track vibration and braking thermal load, requiring high steel purity, internal compactness, fatigue property and dimensional accuracy. Fu’an Heavy Industry holds AAR certification and has supplied wide-gauge bogies for Brazil, North America, Australia and other heavy haul railway projects, including steerable bogie, 40KTE, G1/G2 series.
Application Scope
Main equipment matching for heavy-duty diesel locomotives, wide-gauge locomotives and mining locomotives
Overseas railway EPC projects, new heavy haul railway construction & locomotive renewal in North/South America and Australia
Bogie spare parts replacement and lightweight upgrade of existing locomotives
Custom manufacturing conforming to AAR, UIC, GOST railway standards
2. Manufacturing Capability Overview
We provide one-stop full workflow: digital casting simulation, melting & casting, heat treatment, certified welding repair, CNC precision machining and pre-assembly verification. Special anti-deformation tooling and spatial scaling technology are adopted to solve technical bottlenecks such as thin-wall mould filling and casting distortion.
MAGMA casting simulation: 3D modelling to simulate molten steel filling and solidification, optimize gating, riser and chiller layout, predict shrinkage, porosity and hot cracks to control casting deformation.
Melting & resin sand casting: Electric arc furnace + LF/VD vacuum refining to reduce impurities and gas content. Alkaline phenolic resin sand moulding and core assembly with directional feeding to guarantee dense structure on critical load-bearing zones.
Multi-stage heat treatment: Normalizing, tempering and stress-relief annealing to refine microstructure, eliminate casting residual stress, improve impact toughness and fatigue resistance, and reduce structural deformation.
Certified welding repair: Defect repair welding following AAR railway specifications, with post-weld heat treatment to remove welding stress and preserve fatigue strength.
Large CNC precision machining: Gantry milling and floor boring machines for axle box seat, spring seat, traction seat and brake bracket machining. Strict controls on hole position tolerance and datum flatness.
Pre-assembly & dimension recheck: Verification of mounting interfaces and mating dimensions.
3. Quality Control & Inspection
Full traceable quality management system complying with AAR, UIC and ISO railway casting standards. Our testing laboratory holds CNAS accreditation. Witness inspection by client or third-party inspector is available at defined hold points.
Raw material & melting test: Spectral analysis on molten steel. Mechanical property tests (tensile, yield, impact, hardness) on cast test blocks with full batch traceability.
Nondestructive testing (NDT): 100% UT, MT and PT inspection; RT radiographic inspection applied on critical load-bearing sections to detect internal and surface cracks, complying with AAR acceptance criteria.
Precision dimensional inspection: FARO laser tracker and large CMM for full 3D scanning, verifying hole positional tolerance and datum flatness.
Fatigue test (on request): Fatigue test available according to technical agreement to validate structural reliability under cyclic alternating load.
Complete quality documentation package: Melting records, heat treatment curves, full NDT reports, dimensional inspection reports and material certificates with full traceability.
Final inspection: Visual examination, permanent marking, shot blasting and anti-corrosion primer coating before shipment.
4. Customization Process
Technical discussion & review: Client provides drawings, gauge, axle load and technical specifications. We evaluate material, NDT grade, dimensional tolerance and lead time, then sign the technical agreement.
Quotation & contract signing: Formal quotation after technical confirmation. Contract defines witness inspection, warranty and delivery terms.
Process planning & casting simulation: Internal process development, MAGMA solidification simulation and anti-deformation fixture design.
Production & in-process hold-point inspection: Moulding, melting, casting, heat treatment, welding, rough & finish machining. Key stages open for customer or third-party witness.
Final inspection & pre-assembly verification: Mechanical test, full NDT, 3D dimension scanning and mounting interface validation.
Document handover, packaging & shipment: Transfer of complete quality data package; heavy-duty anti-rust packaging for oversize cargo. Shipment supervision optional.
After-sales service: Technical consultation for assembly and quality response during warranty period.
Note: The above information is released by Angang Heavy Machinery and reviewed by Engineer Song Enyu from PALJET.
Next product:Hydro Turbine Upper CrownPrevious product:Integrally Cast Water Turbine Runner