 Paljet
Hydro Turbine Upper Crown | Large Stainless Steel Casting for Francis Turbine Runner
Detailed Introduction
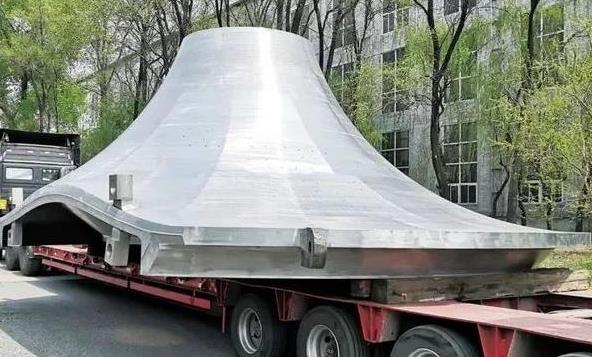
Hydro turbine upper crown, large CA6NM stainless
steel casting for francis turbine runner
1. Product Positioning & Application
Hydro turbine upper crown is the core large pressure-bearing casting for Francis turbine runner. Together with blades and lower ring, it forms the turbine runner. Located at the top of runner and connected with main shaft, the upper crown bears massive hydraulic thrust, alternating hydraulic load and cavitation erosion. It is a critical component of hydropower generating units and directly determines unit stability, efficiency and service life.
Product positioning: OEM large stainless steel / carbon steel hydro turbine upper crown castings, manufactured to IEC, European standards and customer drawings. Available for new hydropower stations and runner retrofitting replacement for overseas hydropower EPC export projects. Both monolithic and segmented casting solutions are available for extra large diameter crowns.
Applications: Francis turbine generating units for large & medium hydropower plants and pumped storage power stations. Target clients: international hydropower EPC contractors, hydropower OEMs and power plant owners. Typical materials: ZG06Cr13Ni4Mo martensitic stainless steel (preferred for cavitation resistance), carbon / low alloy steel, selected according to water head and silt condition.
2. Manufacturing Capability Overview
Our own full-process manufacturing capability for large curved heavy-section hydropower castings: 3D Simulation & Segmented Molding: MAGMA / ProCAST solidification simulation to predict hot spots, shrinkage, distortion and cracking at the transition between hub and conical surface. Resin bonded sand, segmented core assembly and scraper molding process. Zircon sand cores for complex internal cavities to guarantee contour accuracy and prevent mold collapse. Multi-ladle Melting & Pouring: EAF + LF refining + VD vacuum degassing to strictly control S, P, hydrogen, oxygen and inclusions. Multiple ladles melted simultaneously with matched temperature. Bottom gating for steady filling; combined riser design for directional solidification to minimize internal porosity in heavy hub sections. Fettling, Weld Repair & Heat Treatment: Shakeout, gating removal and shot blasting. Defect removal and weld repair with dedicated stainless steel consumables, followed by post-weld stress relief. Full annealing and quenching & tempering to homogenize microstructure, release residual stress and improve fatigue & cavitation resistance. 5-axis CNC Precision Machining: Heavy gantry milling and 5-axis machining centers for finish machining of flanges, shaft holes, blade weld bevels and seal ring seats. Strict control of roundness, concentricity and geometric tolerances. Shop pre-assembly inspection available upon request.
3. Quality Control & Inspection
Full-process QC with third-party witness available to meet strict hydropower acceptance requirements: Raw material inspection: Sampling test for scrap steel, alloys and molding materials. Real-time spectrometer composition monitoring during melting. Visual & dimensional inspection: Visual check + PT penetrant inspection. Full 3D laser scanning to verify outer contour, flanges, holes and curved geometry. Non-destructive testing (NDT, core item): 100% UT ultrasonic inspection on hub, heavy sections and blade bevel areas for internal shrinkage, inclusions and cracks. 100% MT magnetic particle and PT penetrant inspection for surface/subsurface cracks. Re-inspection mandatory after weld repair. Mechanical, metallurgical & corrosion test: Tensile, impact and hardness test on cast-on coupons; metallographic examination. Cavitation test available on demand. Documentation: Material certificate, heat treatment report, UT/MT/PT NDT reports, dimensional report and weld repair records for export clearance and third-party witness.
4. Customization Process
Technical discussion: Client supplies upper crown drawings, material grade, hydraulic load / water head condition, NDT class and dimensional tolerances. Our team reviews casting weight and manufacturing options (monolithic or segmented). Quotation & technical confirmation: Issue casting plan, lead time and commercial quotation. Sign technical agreement to define inspection scope, witness points and acceptance criteria, confirm shop pre-assembly requirement. Process design & pattern fabrication: Solidification simulation, segmented pattern and sand core production. Pattern inspection available on client request. Production & witness: Molding, multi-ladle pouring, heat treatment, weld repair and CNC machining. On-site witness by client or third-party inspectors supported at key stages. Final inspection, coating, export packing & shipment: Complete full NDT, dimensional and material tests and deliver full quality documents. Apply anti-corrosion coating, heavy-duty export packing and arrange ocean freight.
Hydro turbine upper crown is the core large pressure-bearing casting for Francis turbine runner. Together with blades and lower ring, it forms the turbine runner. Located at the top of runner and connected with main shaft, the upper crown bears massive hydraulic thrust, alternating hydraulic load and cavitation erosion. It is a critical component of hydropower generating units and directly determines unit stability, efficiency and service life.
Product positioning: OEM large stainless steel / carbon steel hydro turbine upper crown castings, manufactured to IEC, European standards and customer drawings. Available for new hydropower stations and runner retrofitting replacement for overseas hydropower EPC export projects. Both monolithic and segmented casting solutions are available for extra large diameter crowns.
Applications: Francis turbine generating units for large & medium hydropower plants and pumped storage power stations. Target clients: international hydropower EPC contractors, hydropower OEMs and power plant owners. Typical materials: ZG06Cr13Ni4Mo martensitic stainless steel (preferred for cavitation resistance), carbon / low alloy steel, selected according to water head and silt condition.
2. Manufacturing Capability Overview
Our own full-process manufacturing capability for large curved heavy-section hydropower castings: 3D Simulation & Segmented Molding: MAGMA / ProCAST solidification simulation to predict hot spots, shrinkage, distortion and cracking at the transition between hub and conical surface. Resin bonded sand, segmented core assembly and scraper molding process. Zircon sand cores for complex internal cavities to guarantee contour accuracy and prevent mold collapse. Multi-ladle Melting & Pouring: EAF + LF refining + VD vacuum degassing to strictly control S, P, hydrogen, oxygen and inclusions. Multiple ladles melted simultaneously with matched temperature. Bottom gating for steady filling; combined riser design for directional solidification to minimize internal porosity in heavy hub sections. Fettling, Weld Repair & Heat Treatment: Shakeout, gating removal and shot blasting. Defect removal and weld repair with dedicated stainless steel consumables, followed by post-weld stress relief. Full annealing and quenching & tempering to homogenize microstructure, release residual stress and improve fatigue & cavitation resistance. 5-axis CNC Precision Machining: Heavy gantry milling and 5-axis machining centers for finish machining of flanges, shaft holes, blade weld bevels and seal ring seats. Strict control of roundness, concentricity and geometric tolerances. Shop pre-assembly inspection available upon request.
3. Quality Control & Inspection
Full-process QC with third-party witness available to meet strict hydropower acceptance requirements: Raw material inspection: Sampling test for scrap steel, alloys and molding materials. Real-time spectrometer composition monitoring during melting. Visual & dimensional inspection: Visual check + PT penetrant inspection. Full 3D laser scanning to verify outer contour, flanges, holes and curved geometry. Non-destructive testing (NDT, core item): 100% UT ultrasonic inspection on hub, heavy sections and blade bevel areas for internal shrinkage, inclusions and cracks. 100% MT magnetic particle and PT penetrant inspection for surface/subsurface cracks. Re-inspection mandatory after weld repair. Mechanical, metallurgical & corrosion test: Tensile, impact and hardness test on cast-on coupons; metallographic examination. Cavitation test available on demand. Documentation: Material certificate, heat treatment report, UT/MT/PT NDT reports, dimensional report and weld repair records for export clearance and third-party witness.
4. Customization Process
Technical discussion: Client supplies upper crown drawings, material grade, hydraulic load / water head condition, NDT class and dimensional tolerances. Our team reviews casting weight and manufacturing options (monolithic or segmented). Quotation & technical confirmation: Issue casting plan, lead time and commercial quotation. Sign technical agreement to define inspection scope, witness points and acceptance criteria, confirm shop pre-assembly requirement. Process design & pattern fabrication: Solidification simulation, segmented pattern and sand core production. Pattern inspection available on client request. Production & witness: Molding, multi-ladle pouring, heat treatment, weld repair and CNC machining. On-site witness by client or third-party inspectors supported at key stages. Final inspection, coating, export packing & shipment: Complete full NDT, dimensional and material tests and deliver full quality documents. Apply anti-corrosion coating, heavy-duty export packing and arrange ocean freight.
Note: The above information is released by Angang Heavy Machinery and reviewed by Engineer Song Enyu from PALJET.
Next product:Large flat circular eccentric slag potPrevious product:Integrally Cast Steel Locomotive Bogie Frame
Anshan Leibo Metallurgical Equipment Manufacturing Co., Ltd. Registered Address:Yanlangzhai Village, Dadaowan Town, Qianshan District, Anshan City, Liaoning Province, P.R.China . All Rights Reserved © 2026